How to Test UV Curing Quality from China Top Suppliers?

Time:2026-09-19 Author:Henry
0%

Testing UV curing quality is essential when evaluating products from China’s top suppliers. A glossy surface can look perfect and still hide under-cured material beneath it. Reliable inspection combines measured exposure, physical testing, and supplier documentation.

As photopolymerization expert Dr. Christian Decker has noted, “Curing performance depends on the complete system, not light exposure alone.” This principle guides how to test uv curing quality in a real production environment. Check the lamp’s wavelength, irradiance, exposure time, and distance from the sample. Record every value. Small changes can affect the final result.

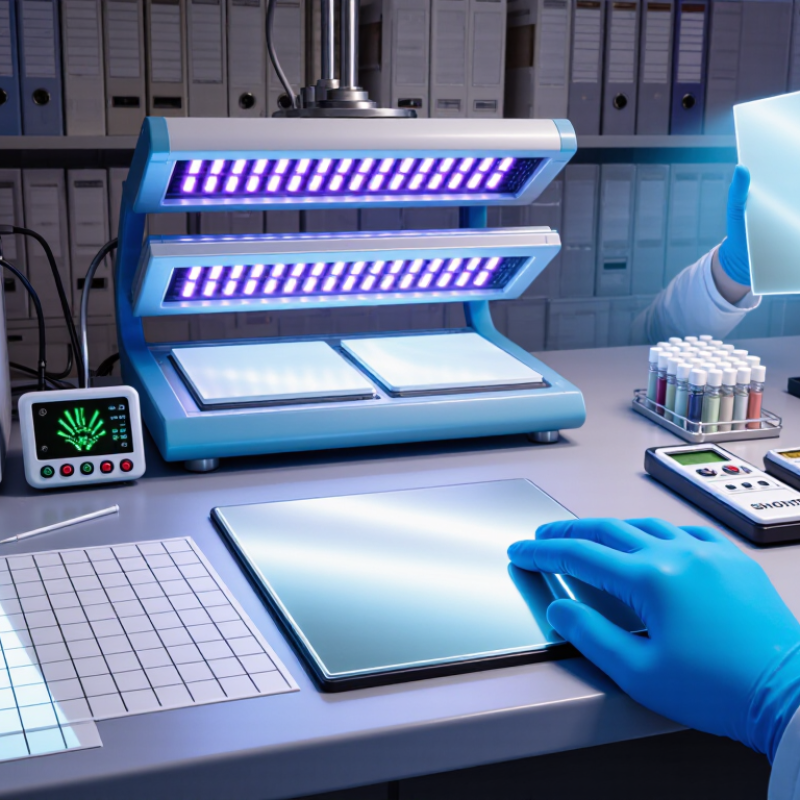
Begin with a tack test using a clean nitrile glove. A properly cured surface should not feel greasy or transfer residue. Measure hardness with a suitable Shore or pencil hardness method. Test adhesion using a cross-hatch grid and tape. Inspect the cut edges under bright light. Look for lifting, cracking, or powdery fragments. For coatings, solvent-rub testing can reveal incomplete polymerization. A stronger laboratory approach uses FTIR to compare residual reactive groups.

Supplier samples deserve repeated testing. One successful panel proves little. Temperature, pigment loading, coating thickness, and lamp aging can change results. I have seen a surface pass a quick touch test but fail after overnight storage. That mistake is easy to make. Ask suppliers for batch records, lamp calibration data, and recommended process windows. Keep your own control samples for comparison. No test is perfect, and visual inspection alone is not enough. A cautious, repeatable method protects product quality and exposes weak process control.
How to Test UV Curing Quality from China Top Suppliers?

Define UV Curing Quality Standards and Acceptance Criteria

UV curing quality starts with written acceptance criteria, not visual confidence. Define lamp wavelength, irradiance, energy dose, exposure time, and substrate temperature. Use a calibrated radiometer for every verification test. For each product, set measurable limits for hardness, adhesion, cure depth, gloss, and color change. A practical specification might require a dose of 800–1,000 mJ/cm² and no detectable surface tack. Keep numbers product-specific.

During supplier qualification, test three samples from different production positions. Measure surface cure with solvent rubs and a defined pass-fail rating. Check adhesion with a crosshatch test after conditioning. Inspect cure depth through a cut section when the coating is thick. Record gloss, color shift, hardness, and temperature near the edges. Acceptance should include repeatability. Every sample should pass, not only the average result. This catches weak lamp zones.

Ask the factory for lamp age, maintenance records, calibration certificates, and batch traceability. I also recommend keeping a retained witness panel from each approved lot. It exposes drift over time. One caution: a perfect first test can mislead. Humidity, coating thickness, pigment load, and line speed can change results. Our early checks once ignored edge curing, and later inspection found soft corners. The criterion was revised to include center and edge readings, with retesting after lamp replacement. Leave room for review.

How to Test UV Curing Quality from China Top Suppliers?

UV curing dose comparison against process acceptance criteria at common UV-A wavelengths.

Acceptance criteria: The measured UV dose should meet or exceed the minimum process dose specified for the selected coating or adhesive. The example readings represent calibrated radiometer measurements collected at five positions across a curing area. Final acceptance should also confirm tack-free curing, adhesion, hardness, color stability, and a dose uniformity of no more than ±10% across the validated area.

Verify Supplier Credentials, Equipment, and Quality Control Systems

How to Test UV Curing Quality from China Top Suppliers?

A reliable supplier should provide verifiable company records, factory details, and production experience. Ask for business licenses, quality certificates, laboratory capabilities, and recent customer references. Confirm that certificates match the legal company name and current factory address. A polished document alone proves little. During supplier reviews, request a live video inspection or an independent factory audit.

Examine the curing equipment closely. Check lamp type, output stability, conveyor speed, curing distance, and cooling control. Ask for calibration records for radiometers and light meters. Request test panels cured under your actual material thickness and production speed. Measure surface tack, adhesion, hardness, cure depth, and appearance after 24 hours. Record every result. Small variations may reveal unstable energy delivery or poor process control.

Tips: Send identical samples to two suppliers. Use the same test method and inspection time. Ask for batch records, incoming material checks, and corrective-action reports. Confirm whether operators monitor lamp intensity during production. One useful detail is the alarm history; repeated temperature or intensity alarms deserve questions. Some suppliers may report excellent first samples but weaker repeat batches. That possibility should not be ignored. My own checks would include a second production trial, because the first result can be unusually careful. Keep photographs, test values, and sample codes together for traceability.

How to Test UV Curing Quality from China Top Suppliers? - Verify Supplier Credentials, Equipment, and Quality Control Systems

Verification Category Data Dimension Recommended Verification Method Typical Acceptance Benchmark Required Evidence Risk Level
Supplier Credentials Quality management system Check the validity, scope, issuing body, and audit status of the quality certificate. Certificate scope covers UV equipment manufacturing, assembly, or related electrical products; certificate is current. Current certificate, registration number, scope statement, and latest surveillance or recertification record. Medium
Production and inspection traceability Review lot numbering, incoming inspection, process records, and final inspection reports. Every delivered unit can be linked to a production lot, key components, inspection results, and shipment date. Sample records for at least three recent production lots with no unexplained gaps. Medium
Calibration management Verify calibration labels and certificates for radiometers, power meters, thermometers, and dimensional tools. Calibration is valid at the time of testing; measurement uncertainty and traceability are documented. Calibration interval commonly controlled at 6–12 months, according to instrument use and risk. High
UV Equipment Wavelength output Measure the spectral output or verify the LED module specification with an independent optical measurement. Measured peak wavelength remains within approximately ±5 nm of the process requirement. Spectral measurement report, LED module specification, and test condition record. High
UV irradiance Measure irradiance at the actual working distance using a suitable radiometer. Measured value meets the process specification; a common industrial range is approximately 0.5–10 W/cm² depending on the application. Radiometer model, measurement location, working distance, warm-up time, and reading history. High
UV dose and exposure time Calculate dose using irradiance multiplied by exposure time and confirm it with a dose measurement where available. Dose is within the coating or adhesive supplier’s validated process window; the calculation uses consistent units. Record dose in J/cm² and exposure time in seconds; do not rely on exposure time alone. High
Irradiance uniformity Measure multiple points across the effective curing area at the actual production distance. Point-to-point variation is typically controlled within ±10% for demanding curing processes, unless the process specification allows more. Grid map showing center, edges, corners, measurement date, and instrument identification. High
Curing Quality Control Surface cure and tack-free condition Inspect the cured surface under controlled lighting and perform a defined rub or tack test. No unacceptable surface tack, transfer, smearing, or visible uncured film under the approved test method. Signed test record, product lot, coating or adhesive lot, UV dose, and operator identification. High
Adhesion after curing Use a cross-cut or pull-off adhesion test appropriate to the coating and substrate. Acceptance level is defined before production; for cross-cut testing, an agreed rating such as ISO 2409 Class 0–1 may be specified when suitable. Test photographs, rating, substrate preparation details, curing parameters, and environmental conditions. High
Cure depth or through-cure Inspect a cross-section or use a validated hardness, solvent-resistance, or mechanical test for the material. No soft or liquid layer remains below the surface; the measured cure depth meets the product specification. Cross-section images or test results from thin, standard, and maximum specified material thicknesses. High
Temperature control Record part temperature during curing using a calibrated contact or non-contact thermometer. Temperature remains below the substrate, coating, adhesive, or component limit; the process does not cause warping or discoloration. Temperature profile, cooling method, conveyor speed, lamp setting, and maximum recorded temperature. Medium
Quality Control System Process capability and repeatability Run repeated samples under identical settings and analyze irradiance, dose, and cure-test results. Results remain within the approved process window with no unexplained trend or excessive variation. Minimum three repeated readings per condition and a documented reaction plan for out-of-control results. High
Preventive maintenance Review cleaning, cooling, LED output checks, replacement intervals, and maintenance sign-off records. Maintenance frequency is risk-based and records show completion before overdue dates. Maintenance schedule, completed checklists, spare-parts records, and post-maintenance verification results. Medium
Nonconformance and corrective action Review recent nonconformance reports and verify root-cause analysis, containment, and effectiveness checks. Issues are documented, affected lots are controlled, and corrective actions are verified before closure. Anonymized corrective-action records, closure dates, responsible personnel, and effectiveness evidence. High
Evaluation rule: Approve the supplier only when wavelength, irradiance, dose, uniformity, curing performance, calibration, and traceability records meet the pre-defined process requirements. Acceptance limits should be finalized with the coating, ink, adhesive, or resin specification before production release.

Inspect UV Curing Materials, Machines, and Production Conditions

How to Test UV Curing Quality from China Top Suppliers?

Inspect UV curing materials, machines, and production conditions before approving any supplier. Request the exact resin, photoinitiator, coating thickness, and recommended wavelength. Record batch numbers. Small formula changes can alter surface cure, adhesion, and yellowing.

Measure irradiance in mW/cm² and dose in mJ/cm² at the actual working distance. Do not trust the display alone. Use a calibrated radiometer, because lamp aging and reflector contamination reduce delivered energy. The International Commission on Illumination identifies measurement geometry as critical for repeatable optical testing. Smithers’ 2023 UV LED curing market analysis also highlights wavelength control and process consistency as major quality drivers.

Inspect the machine physically. Check LED uniformity across the conveyor, cooling-water temperature, belt speed, shielding, and emergency controls. Test three positions: center, left edge, and right edge. Cure identical samples under identical settings, then compare tack-free time, pencil hardness, cross-hatch adhesion, gloss, and solvent resistance. ASTM D3359 supports cross-cut adhesion evaluation, while ASTM D3363 is commonly used for pencil hardness. Keep the samples for seven days; early results can mislead. I once treated a hard surface as fully cured. The cross-cut test later exposed weak interlayer adhesion. Production conditions deserve equal attention. Dust, humidity, substrate temperature, and inconsistent coating thickness can quietly damage repeatability. Photograph every setup and preserve the raw readings. Supplier claims need evidence.

Perform Tests for Cure Depth, Adhesion, Hardness, and Surface Finish

When evaluating UV curing quality from China’s top suppliers, test actual production samples, not only certificates. Record lamp wavelength, irradiance, exposure time, and material batch. Cure depth can be checked by cutting a cured section and measuring the solid layer with a microscope. A thin uncured zone may feel harmless, but it can weaken bonding later.

Adhesion testing should match the product surface. Use a cross-hatch test on coated panels, then apply standardized tape and inspect lifted squares. Check hardness with a pencil hardness method or a calibrated durometer. Do not judge hardness by touch alone. For surface finish, inspect gloss, orange peel, bubbles, tackiness, and visible streaks under consistent lighting. A gloss meter adds useful data, although visual inspection still catches defects that instruments miss.

Tips: Test at least three samples from separate batches. Keep lamp distance and temperature stable. Ask suppliers for test conditions, not just pass results. We once accepted a smooth panel that later showed poor edge curing; the center had received more energy. That mistake reinforced an important lesson: measure edges, corners, and hidden surfaces. Repeat testing after storage, because some coatings harden initially but lose adhesion or develop surface haze over time. Record every result with photos, readings, and operator notes. Perfect repeatability is difficult, but unexplained variation deserves investigation.

Review Test Results, Certifications, and Supplier Quality Records

Testing UV curing quality from China’s top suppliers requires more than checking whether a sample feels dry. Review the supplier’s test results for irradiance, exposure dose, wavelength, curing speed, surface tack, hardness, and adhesion. Ask how each result was measured. A report should identify the lamp type, test distance, material thickness, batch number, and equipment calibration date. Small details matter. We once accepted a curing report with strong results, but it used a thinner sample than our production material. The comparison was misleading.

Certifications can support supplier credibility, but they do not replace technical verification. Check the certificate scope, issuing body, validity period, and covered manufacturing site. Quality systems such as ISO 9001 may show process discipline, while product-specific certifications should match the equipment and application. Request supplier quality records, including incoming inspection data, final inspection reports, calibration logs, nonconformance records, corrective actions, and batch traceability. Reliable suppliers should provide controlled documents without avoiding difficult questions.

Run an independent trial when possible. Measure curing performance at the intended production speed and temperature. Compare results across several batches, not one perfect sample. Review dose consistency across the working area, especially near the edges. Keep photos, test conditions, and raw readings in your evaluation file. The review may still contain uncertainty. Supplier data can be accurate yet incomplete. That is why repeated testing, clear acceptance limits, and direct technical discussions remain essential.

FAQS

What should a UV curing acceptance specification include?

Define wavelength, irradiance, dose, exposure time, and substrate temperature. Set product-specific limits for hardness, adhesion, cure depth, gloss, and color change. A practical dose may be 800–1,000 mJ/cm². Keep it measurable.

How should curing energy be verified?

Measure irradiance in mW/cm² and dose in mJ/cm². Use a calibrated radiometer at the actual working distance. Do not rely only on the machine display. Lamp aging and dirty reflectors can reduce delivered energy.

How many samples should be tested during supplier qualification?

Test three samples from different production positions. Check the center, left edge, and right edge. Every sample should pass the limits. An average result can hide a weak lamp zone.

Which tests can confirm surface and internal curing?

Use solvent rubs to evaluate surface cure and tack. Use cross-cut adhesion testing after conditioning. Inspect a cut section when the coating is thick. Seven days can reveal delayed failures.

What machine conditions need inspection?

Check LED uniformity, cooling-water temperature, belt speed, shielding, and emergency controls. Record the working distance and exposure settings. Dust, humidity, and substrate temperature can change results quietly. Production details matter.

Which material information should a supplier provide?

Request the exact resin, photoinitiator, coating thickness, and recommended wavelength. Record every material batch number. Small formula changes can affect adhesion, yellowing, and surface cure. Do not assume matching labels mean matching performance.

Why should edge curing receive special attention?

Edges may receive less energy than the center. Measure hardness, gloss, temperature, and tack near the edges. Our early checks ignored soft corners. The acceptance criteria had to change.

What records should be retained after approval?

Keep lamp age, maintenance records, calibration certificates, batch details, photographs, and raw readings. Retain one witness panel from each approved lot. It can reveal curing drift later. A perfect first test can mislead.

Conclusion

Testing UV curing quality from top suppliers in China requires a clear and consistent evaluation process. First, define curing standards and acceptance criteria for factors such as cure depth, adhesion, hardness, appearance, and durability. Then verify the supplier’s experience, production equipment, inspection methods, and quality control system. A reliable supplier should be able to provide transparent process information, qualified personnel, and complete quality records.

To understand how to test uv curing quality, inspect the raw materials, UV lamps or curing machines, operating conditions, and production environment. Conduct practical tests for cure depth, coating adhesion, surface hardness, uniformity, and surface finish under controlled conditions. Finally, compare the test results with your requirements, review relevant certifications and inspection reports, and confirm that the supplier maintains consistent quality throughout production. This approach helps reduce performance risks and supports a more informed purchasing decision.
Henry

Henry

Henry is a dedicated marketing professional with a profound expertise in the company's offerings. With years of experience in the industry, he possesses an impressive understanding of the market dynamics and consumer behaviors that drive success. Henry is committed to sharing his insights through......